


Mirror EDM Machine
Your Professional Mirror EDM Machine Supplier
SUZHOU HANQI CNC EQUIPMENT CO., LTD. specializes in the manufacturing and customization of a wide range of precision CNC electric discharge machines (EDM) and CNC wire EDM cutting machines (WEDM). Hanqi CNC machines (EDM/WEDM) are extensively utilized across various industries, such as mold manufacturing, automotive production, semiconductor technology, medical equipment, electronics, electrical engineering, hardware, and plastics.
Quality Certification
The company has obtained ISO 9001 quality management system certification and has been recognized as a national "High-Tech Enterprise" and a "Provincial Private Technology Enterprise."
Strong Strength
Currently, the company operates a modern factory spanning over 20 acres within the Suzhou High-Tech Zone, Jiangsu Province, with a total built-up area exceeding 20,000 square meters.
Independent Research and Development Capabilities
The company possesses independent design and R&D capabilities and holds two national invention patents.
24/7 Online Support
Professional customer service is available around the clock. If you encounter any problems in the use of machine tools, we will provide you with more intuitive solutions. Provide comprehensive and systematic help in terms of technology.
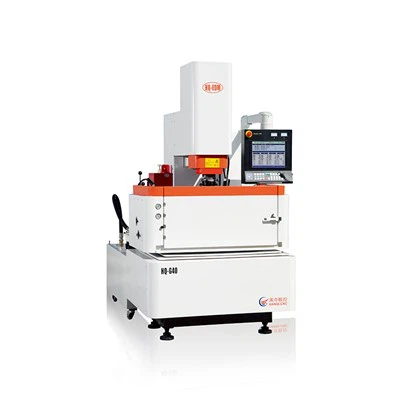

Product Categories



Parameter
|
Machine Size |
Mm |
1450x 1350 x 2400 |
|
Machine Weight |
KG |
2800 |
|
Work Area |
|
|
|
X, Y, Z-Stroke |
Mm |
400x 300x 320 |
|
Table Size |
Mm |
680x 420 |
|
Maximum Load-Bearing Capacity Of Table |
KG |
500 |
|
Dimensions Of Working Fluid Tank |
Mm |
980x 650x 400 |
|
Maximum Distance Between Electrode Plate And Table |
Mm |
600 |
|
Pulse Power |
|
|
|
Power Input |
Kw |
9 |
|
Maximum Machining Current |
A |
50 |
|
Maximum Electrode Weight |
KG |
50 |
|
Maximum Processing Efficiency |
MM3/min |
≥500 |
|
Drive Mode |
|
Full Digital AC servo |
|
Minimum Electrode Loss |
|
0.05% |
|
Surface Roughness |
Um |
RA ≤0.08 |
|
Minimum Drive Unit |
Um |
1 |
|
Number Of Coordinates |
|
60 |
|
Input Mode |
Touch screen, USB |
|
|
Display Mode |
15-inch TFT-LCD, CRT |
|
|
Compensation Of Each Axis |
Each axis carries on the step distance error compensation, the gap compensation respectively |
|
|
Resolution Of Each Axis |
0.4 |
|
|
Process Standard |
Steel/steel, fine steel, graphite/steel, fine copper-tungsten/steel, Copper-tungsten/cemented carbide copper/aluminum, graphite/titanium |
|
|
Interpolation Method |
Straight line, arc, spiral line, bamboo gun |
|
|
Processing Discharge Conditions |
Register function 1000 conditions (C000-C999) |
|
|
Maximum Number Of Control Axes |
Three axis three linkage (standard) four axis four linkage (optional) |
|
|
Input Range |
+ 9999.999 ~ -9999.999 |
|
Advantages of Mirror EDM Machine
Accuracy
Achieves tolerances as tight as a few microns.
Versatility
Machining hard and delicate materials with precision
Low Stress
No mechanical stress, with the material intact.
Automation
CNC Electrical Discharge Machines EDM equipment save labor and increase productivity.
Aerospace Components
An aerospace part has many features that can’t be produced with some common cutting tools, this is where EDM machining is useful. Tight deep hole requirements, thin slots, sharply squared holes, and turbine rotor discs are just some problematic features that EDM machining can create.
Small Hole Drilling
Irrespective of the hardness of the material, electrical discharge machining is a fast and innovative way to drill precise, tiny, deep holes in it. Electrical discharges are directed onto the material using a brass electrode tube during the hole drilling procedure. This aids in producing holes of different tiny diameters.
Medical Components
EDM machined products are ideal for producing different medical implant components because they do not produce burrs during manufacturing.


Die Casting
Applications involving die-making also benefit significantly from EDM. Creating extremely precise dies requires a high degree of accuracy. These dies have deep ribs, sharp internal corners, and other detailed features.
Components Disintegration
Metal that has become stuck inside a workpiece and cannot be removed using conventional methods is also removed using an EDM machine. Destroying or extracting the material is necessary to disintegrate the stuck components.
Injection Molding
EDM is usually required to achieve the proper mold dimension, depth, and shape. Mold makers use it as their primary injection molding process. In this instance, wire EDM is the primary type.
Points To Pay Attention To In The Process Of Mirror EDM Machine
A reasonable distance must be maintained between the tool electrode and the workpiece electrode. Within this distance range, the pulse voltage can continuously break down the medium and generate spark discharge, and it can also meet the requirements of deionization of the medium and discharge of corrosion products after the spark channel is extinguished.
The pulse discharge needs to be repeated many times, and the multiple pulse discharges are dispersed in time and space. This has two meanings:
● One of the two adjacent pulses in time does not form a channel at the same point.
● Second, if the pulse discharge occurs concentratedly in a certain area within a certain period of time, the pulse discharge should be transferred to another area within another period of time. Only in this way can carbon deposition be avoided, thereby avoiding arcing and local burns.
The pulse energy density delivered between the two electrodes should be large enough. After the spark channel is formed, the pulse voltage does not change much, so the current density of the channel can characterize the energy density of the channel. The energy density is large enough to locally melt or vaporize the processed material, thereby forming a corrosion mark (pit) on the surface of the processed material to realize EDM.
The galvanic corrosion products after the pulse discharge can be discharged to the outside of the discharge gap in time, so that the repetitive discharge can be carried out smoothly. In the production practice of EDM, the above process is completed in two ways.
Order Process

Packaging and Shipping
|
Packaging |
Standard Seaworthy Packing: Wooden Case For different shipping methods and destinations, we will suggest different packaging. If you have any requirement for the packaging, please let me know during enquiry. |
|
Shipping |
We offer our clients one-stop service.The shipping tool can be by sea, by air or by train. It depends on the destination of our products. And we will suggest you the min. cost and min. damage of the products. |
Other Services
|
Delivery Details |
25-30 days |
|
MOQ |
1 set |
|
Port |
Shanghai or any China port |
|
Payment Method |
L/C or T/T |
Our Factory
Our Certificate


FAQ
As one of the leading mirror EDM machine manufacturers in China, we warmly welcome you to buy discount mirror EDM machine from our factory. All customized machines are with high quality and low price.
fully cnc mirror servo high precision edm machine, fully cnc mirror servo edm machine